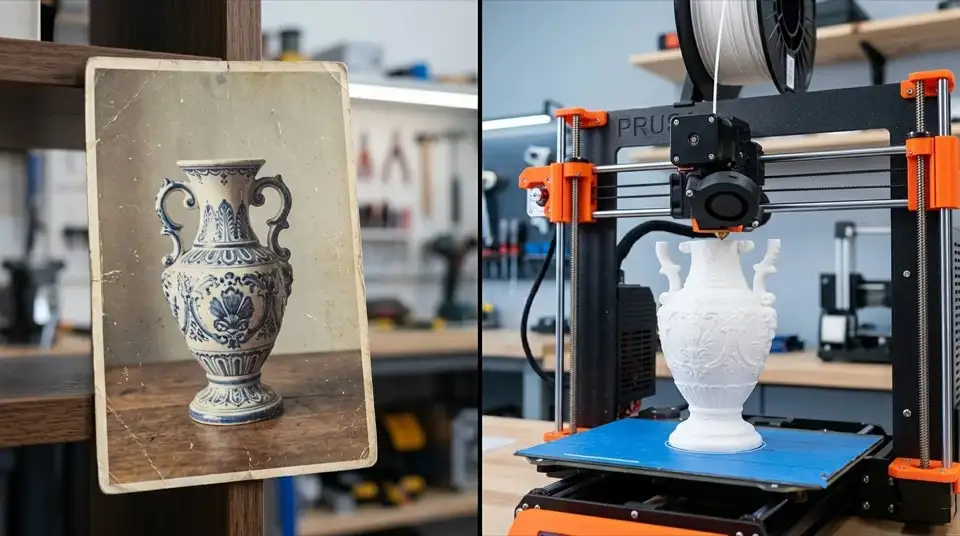
Image to 3D Model for 3D Printing: Complete Workflow Guide (2026)
Turn any photo into a 3D-printable model. Covers AI tool selection, mesh repair in Blender, STL export settings, slicer configuration, and troubleshooting common print failures. Works with TRELLIS 2, Meshy AI, and Tripo AI.
Last updated: May 3, 2026
You generated a 3D model from a photo using an AI tool. It looks great on screen. But when you try to print it, the slicer throws errors about non-manifold geometry, the model has holes, and the print fails halfway through.
This is the gap most "image to 3D" guides ignore. AI tools optimize for visual quality, not printability. This guide covers the complete pipeline — from choosing the right AI tool to holding a finished print in your hands.
The Problem: AI Models Aren't Print-Ready
AI image-to-3D tools (TRELLIS 2, Meshy AI, Tripo AI, and others) are trained to produce models that look good on screen. 3D printers have different requirements:
| AI Model Property | 3D Printing Requirement |
|---|---|
| Visual appearance matters most | Structural integrity matters most |
| 50k–2M polygons is fine | 100k–250k polygons (FDM) or 500k–1.5M (resin) |
| Open surfaces and thin walls are OK | Must be watertight with minimum 0.8mm walls (FDM) |
| Arbitrary scale | Precise dimensions in mm |
| Flipped normals don't affect rendering | Flipped normals cause missing layers |
Models with more than 5% self-intersecting geometry have a 40% higher failure rate in standard FDM printing. Most AI-generated models need some preparation before they're printable.
Step 1: Choose the Right AI Tool for 3D Printing
Not all AI tools produce equally printable models. Here's how they compare for print-specific output:
| Tool | Watertight Rate | Best Export Format | Print-Specific Features | Print-Readiness Score |
|---|---|---|---|---|
| Meshy AI | ~55% fully watertight | STL, 3MF | One-click "Send to Bambu", 97% slicer pass rate | 5/6 |
| Hitem3D | Highest (1536³ resolution) | STL, OBJ | Print-first architecture, minimal repair needed | 5/6 |
| Tripo AI | Good (auto-repair built in) | STL, 3MF, OBJ | Auto-fixes non-manifold geometry before export | 4/6 |
| TRELLIS 2 | Good | GLB (→ STL) | Configurable decimation, remesh option | 4/6 |
| Rodin AI | Lowest | GLB, OBJ | None — requires significant Blender cleanup | 1/6 |
Recommendation by use case:
| What You're Printing | Best Tool | Why |
|---|---|---|
| Figurines and characters | Meshy AI or Hitem3D | Highest watertight rate, hand-optimized for collectibles |
| Quick prototypes | Tripo AI | Fastest generation + built-in auto-repair |
| Free / open source | TRELLIS 2 | MIT license, local control, customizable output |
Generate a 3D-printable model from your photo — try it free
Step 2: Generate the Model with Printing in Mind
Choose the Right Input Image
The quality of your print starts with the source image. For 3D printing, the ideal input has:
- A single, clearly defined subject — no overlapping objects
- Clean background — solid color or transparent
- Even lighting — no harsh shadows that confuse depth estimation
- View from the front or 3/4 angle — shows the most detail
- Subject fills most of the frame — maximizes detail
Best Objects to Print from AI
Easy to print (high success rate):
- Figurines and character models
- Vases and containers
- Simple props and decorative objects
- Organic shapes (animals, plants)
Difficult to print (expect issues):
- Mechanical parts with precise dimensions
- Objects with thin features (antennae, hair, fingers)
- Large overhangs (>45°)
- Flat, geometric shapes (AI struggles with precision)
TRELLIS 2: Export Settings for Printing
If using TRELLIS 2 locally, configure the export for printability:
glb = o_voxel.postprocess.to_glb(
    # ... mesh data ...
    decimation_target = 250000,  # Target ~250k faces for FDM
    texture_size     = 4096,
    remesh           = True,     # Enable remeshing for cleaner topology
    remesh_band      = 1,
)
Important: Setting decimation_target below 50,000 can cause GLB export errors. For very low-poly prints, export at a higher resolution first, then decimate in Blender.
On our platform, simply select STL as the export format. The model is automatically optimized for printing compatibility.
Step 3: Export in the Right Format
| Format | Best For | Color Support | File Size | Recommended |
|---|---|---|---|---|
| STL | Universal compatibility (all slicers) | None | Large | Most prints |
| 3MF | Bambu Studio, PrusaSlicer | Yes (color, materials) | Compact | Multi-color prints |
| OBJ | Intermediate editing | Yes (via .mtl) | Medium | Before mesh repair |
When to use STL: Single-color prints, maximum slicer compatibility. This is the safest choice.
When to use 3MF: If you use a Bambu Lab printer, 3MF preserves color data and print settings. Meshy AI is currently the only AI tool that exports 3MF natively.
Avoid GLB for printing: GLB is optimized for real-time rendering, not printing. Always convert to STL or 3MF first.
Step 4: Validate and Repair the Mesh
Before sending to the slicer, check your model for common issues. Even "watertight" models from AI tools can have subtle problems.
Quick Check: Blender 3D Print Toolbox
- Install:
Edit > Preferences > Add-ons→ search "3D Print" → enable - Open the panel: Press
Nin the 3D viewport → click 3D-Print tab - Click Check to analyze your model
- Review any highlighted issues:
- Non-manifold edges — edges shared by more than 2 faces
- Intersecting faces — faces that pass through each other
- Degenerate geometry — zero-area faces or duplicate vertices
- Flipped normals — faces pointing the wrong direction
Quick Fixes
For non-manifold geometry:
- Select all (
A) →Mesh > Clean Up > Make Manifold - Or use
Select > Select All by Trait > Non-Manifoldto find and fix manually
For thin walls:
- Add a Solidify modifier with a thickness of 1.5–2mm
One-click repair alternatives:
- Windows 3D Builder: Import model → accept the auto-repair prompt (Windows only)
- Formware Online STL Repair: Free web tool at formware.co/onlinestlrepair
- Bambu Studio: Built-in "Fix Model" function (Windows version)
Decimation (Reducing Polygon Count)
AI models often have 200k–2M polygons. For FDM printing, reduce to 100k–250k:
In Blender:
- Select the model
Modifiers→ Add Decimate modifier- Set Ratio or Face Count to your target
- Apply the modifier
In MeshLab:
Filters > Remeshing > Simplification: Quadric Edge Collapse Decimation- Set target polygon count
- Preview and apply
Step 5: Hollow Out Large Models (Save Material)
For models larger than 50mm in any dimension, hollowing out saves 50–70% of material.
Using Meshmixer
- Import your repaired STL
- Select all (
Ctrl+A) Edit > Make Solid- Set Solid Type to "Hollow"
- Set Wall Thickness to 1.5–2mm (FDM) or 1–2mm (resin)
- Click Update to preview, then Accept
- Add drainage holes:
Edit > Hollow→ enable "Drain Holes"
Critical for resin printing: Models printed in resin must have drainage holes. Uncured resin trapped inside creates pressure that can crack the model during post-processing.
Using Blender
- Add a Solidify modifier with negative offset
- Or use the Remesh modifier with Voxel mode to create a shell
- Add a cylinder mesh and use Boolean > Difference to create drainage holes
Step 6: Slice and Print
Recommended Slicer Settings for AI Models
| Setting | Detail Priority | Speed Priority |
|---|---|---|
| Layer height | 0.12–0.16mm | 0.20–0.28mm |
| Infill | 15–20% Gyroid | 10–15% Grid |
| Supports | Tree supports | Standard supports |
| Adhesion | Brim (4–8mm) | Brim (3mm) |
| Wall loops | 3–4 | 2–3 |
Model Orientation Tips
How you place the model on the build plate significantly affects print quality:
- Largest flat surface faces down — maximizes bed adhesion
- Most detailed surfaces face up — avoids support marks on detailed areas
- Minimize overhangs — rotate to reduce surfaces exceeding 45° from vertical
- Orient overhangs toward the cooling fan — improves overhang quality
FDM vs Resin Printing
| Factor | FDM | Resin (SLA/DLP) |
|---|---|---|
| Best for | Large display models, functional prototypes | Miniatures, figurines, jewelry |
| Layer height | 0.08–0.28mm | 0.025–0.05mm |
| Min wall thickness | 0.8mm | 0.3mm |
| Polygon budget | 100k–250k | 500k–1.5M |
| Post-processing | Remove supports, sand | Wash, cure, remove supports |
| Material cost | Low ($15–30/kg) | Higher ($30–60/L) |
For figurines and detailed models, resin printing is strongly recommended. The 5–10x finer layer height captures details that FDM simply cannot reproduce.
Step 7: Troubleshooting Common Print Failures
| Problem | Cause | Fix |
|---|---|---|
| Slicer shows "non-manifold" error | Gaps or internal faces in mesh | Run Make Manifold in Blender, or use 3D Builder auto-repair |
| Missing layers or gaps in print | Flipped normals | Recalculate normals: Mesh > Normals > Recalculate Outside |
| Model too fragile | Thin walls (<0.8mm) | Add Solidify modifier with 1.5mm minimum thickness |
| Slicer crashes or freezes | Too many polygons (>2M) | Decimate to under 500k before importing |
| Stringy surface on overhangs | Insufficient cooling + large overhang | Use tree supports + increase cooling fan speed |
| Warping at base | Poor bed adhesion + large flat surface | Add brim (8mm), use textured PEI sheet |
| Supports impossible to remove | Supports fused to detailed surfaces | Switch to tree supports, reduce support density |
Complete Workflow Summary
1. Prepare input image
   Clean background, single subject, good lighting
   ↓
2. Generate 3D model (TRELLIS 2 / Meshy / Tripo)
   Export as STL or 3MF
   ↓
3. Validate mesh (Blender 3D Print Toolbox)
   Check: watertight, normals, polygon count
   ↓
4. Repair (if needed)
   Make Manifold, fix normals, decimate to 100k-250k
   ↓
5. Hollow out (optional, saves 50-70% material)
   1.5-2mm walls, add drainage holes
   ↓
6. Slice
   Layer height: 0.12-0.20mm
   Infill: 15-20% Gyroid
   Supports: Tree supports
   Adhesion: Brim
   ↓
7. Print
   ↓
8. Post-process
   Remove supports, sand, prime, paint
Recommended Tools Summary
| Tool | Purpose | Cost |
|---|---|---|
| Blender | Mesh validation, repair, decimation | Free |
| MeshLab | Advanced mesh processing | Free |
| Meshmixer | Hollowing, pattern creation | Free |
| Windows 3D Builder | One-click auto-repair | Free (Windows) |
| Formware Online Repair | Browser-based STL repair | Free |
| Bambu Studio | Slicing (Bambu Lab printers) | Free |
| Cura | Slicing (Ultimaker and others) | Free |
| PrusaSlicer | Slicing (Prusa and others) | Free |
Generate a 3D-Printable Model Now
Our platform lets you generate and export STL files directly — no GPU or Python setup required.
Upload Your Photo — Get a Printable 3D Model
| Approach | Local Setup | Our Platform |
|---|---|---|
| Setup time | 2–4 hours | 0 minutes |
| GPU required | NVIDIA 16GB+ | None |
| Export format | GLB → convert to STL | Direct STL export |
| Mesh quality | Depends on parameters | Optimized for printing |
Related articles:
- How to Turn an Image into a 3D Model: broader guide covering all conversion methods
- How to Use TRELLIS 2: complete usage guide with parameter tuning
- Best Image to 3D Models on HuggingFace: compare open-source models
- Best AI 3D Model Generator: tool comparison for all use cases
Author

3D technology specialists focused on AI-powered 3D model generation, format conversion, and browser-based 3D rendering. We test and review 3D tools so you don't have to.
Categories
More Posts
- Is Trellis 2 Free? Official Pricing & Free Usage Guide (2026)The Trellis 2 model is MIT-licensed and free to run. The official platform is paid, from $19/month. Real plans, credit math, and a wrapper checklist.
- Trellis 2 vs Hunyuan 3D: Complete Comparison (2026 Benchmarks)Official benchmarks, resolution ceilings, license terms, and real outputs — which AI 3D model fits your workflow in 2026.
- Godot MCP: Complete Setup Guide & Server Comparison (2025)What Godot MCP is, which of the four main implementations to pick, step-by-step setup for Claude Code, Codex and Cursor, plus the errors you'll actually hit.